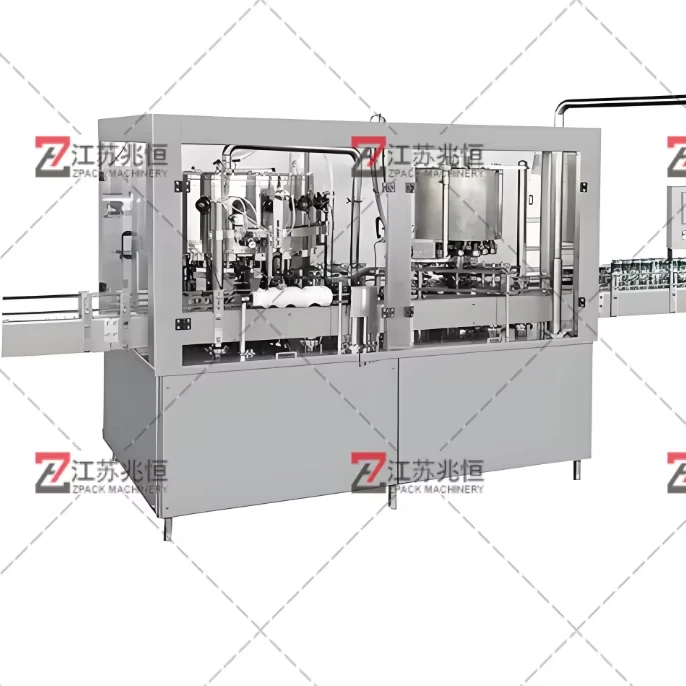
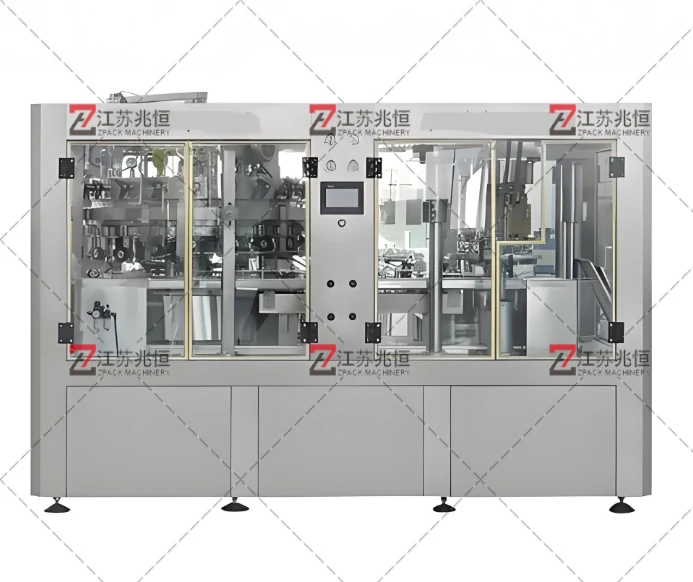
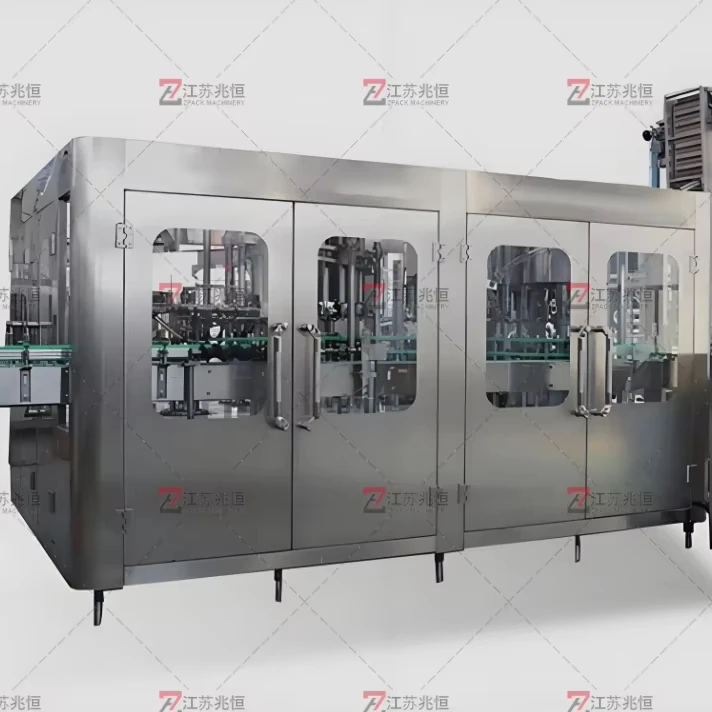
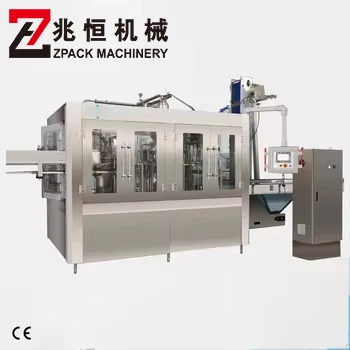
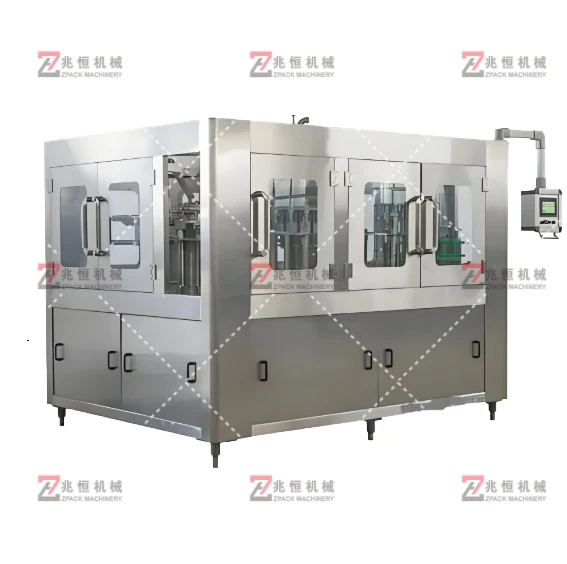
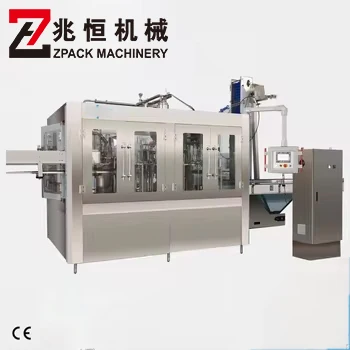
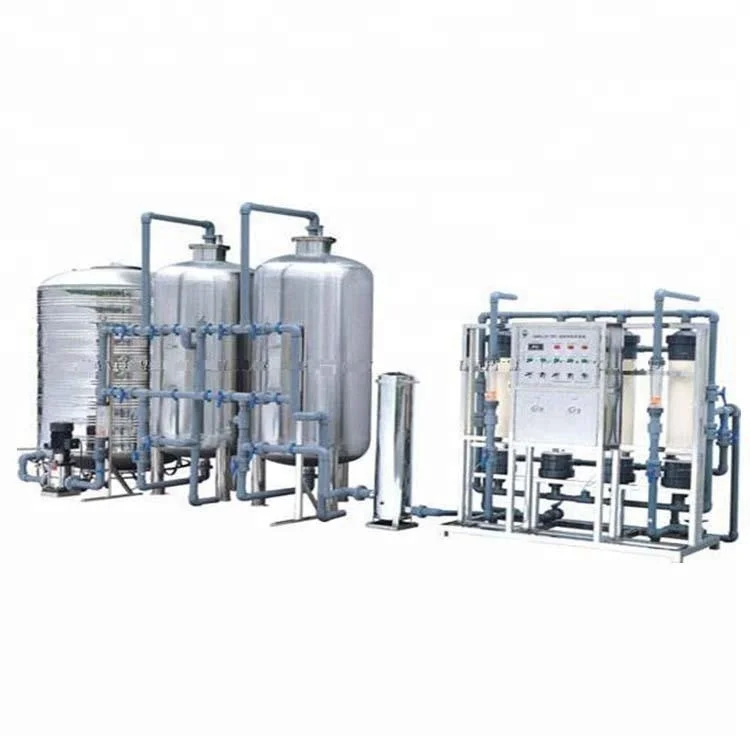
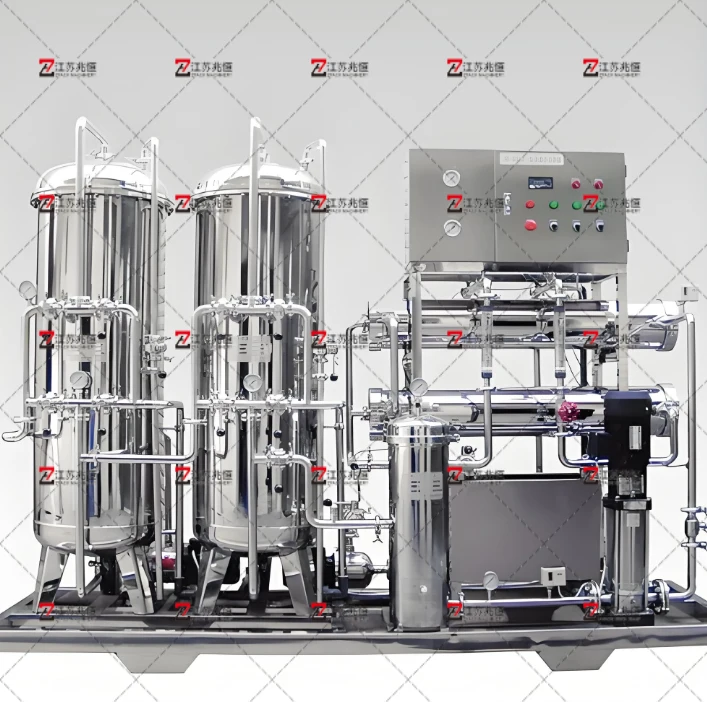
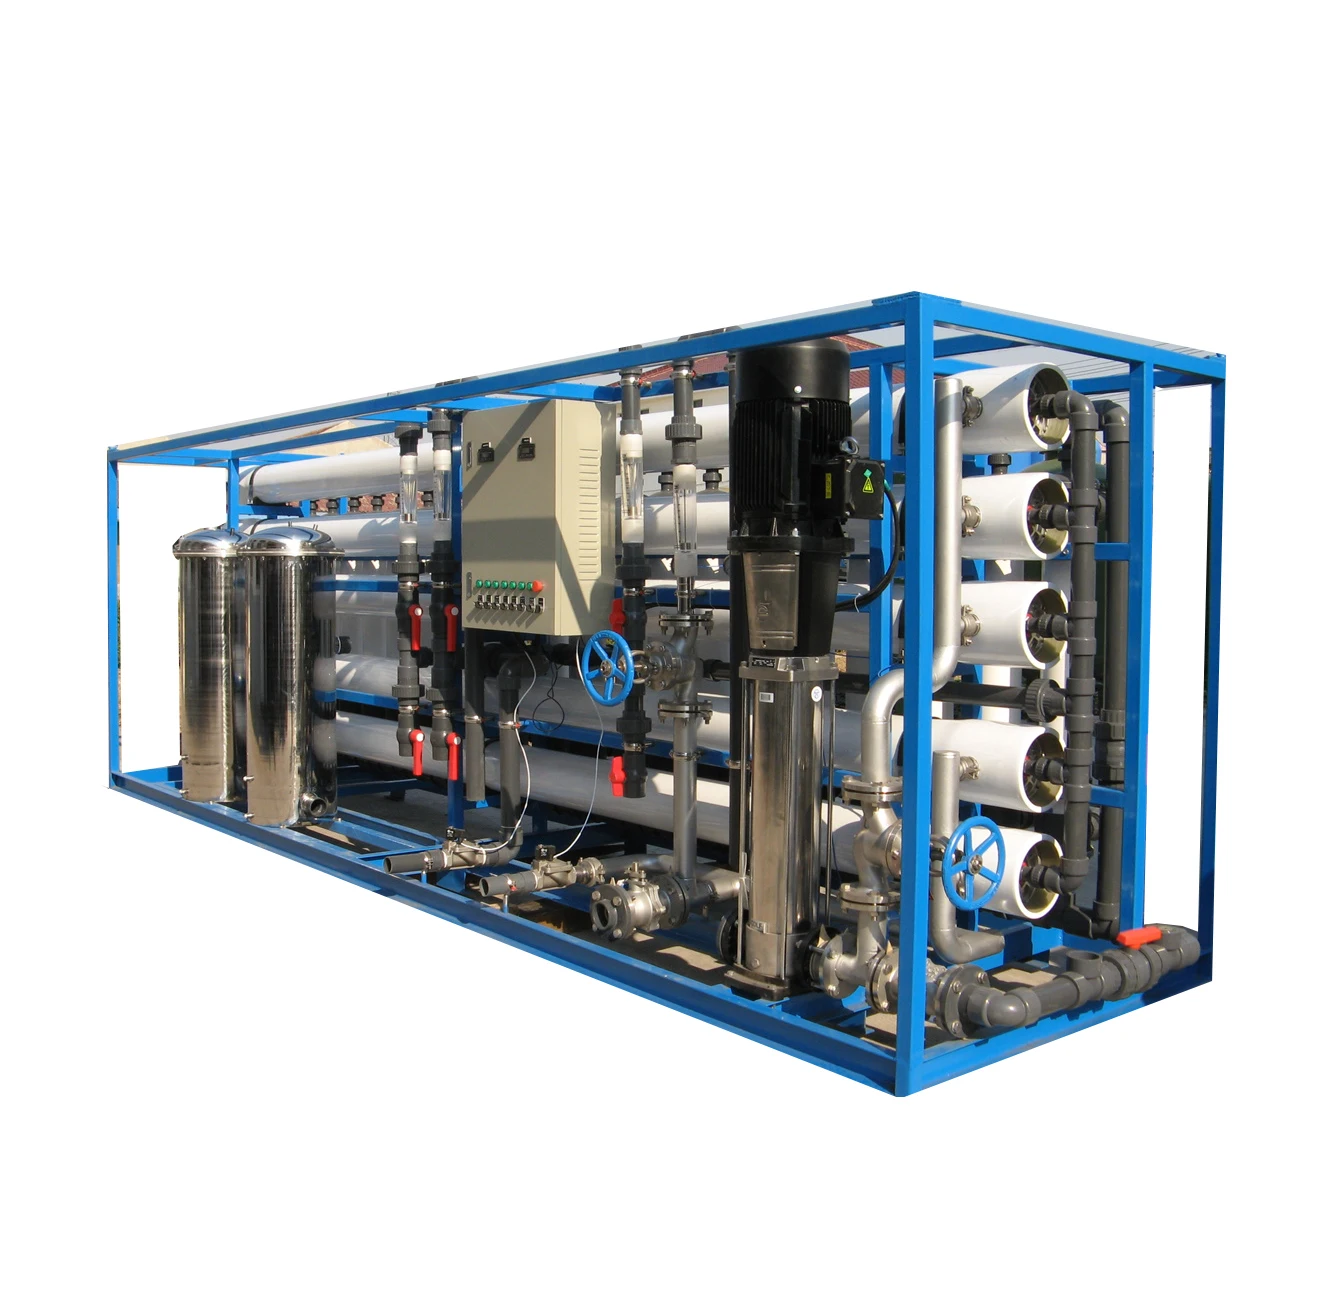
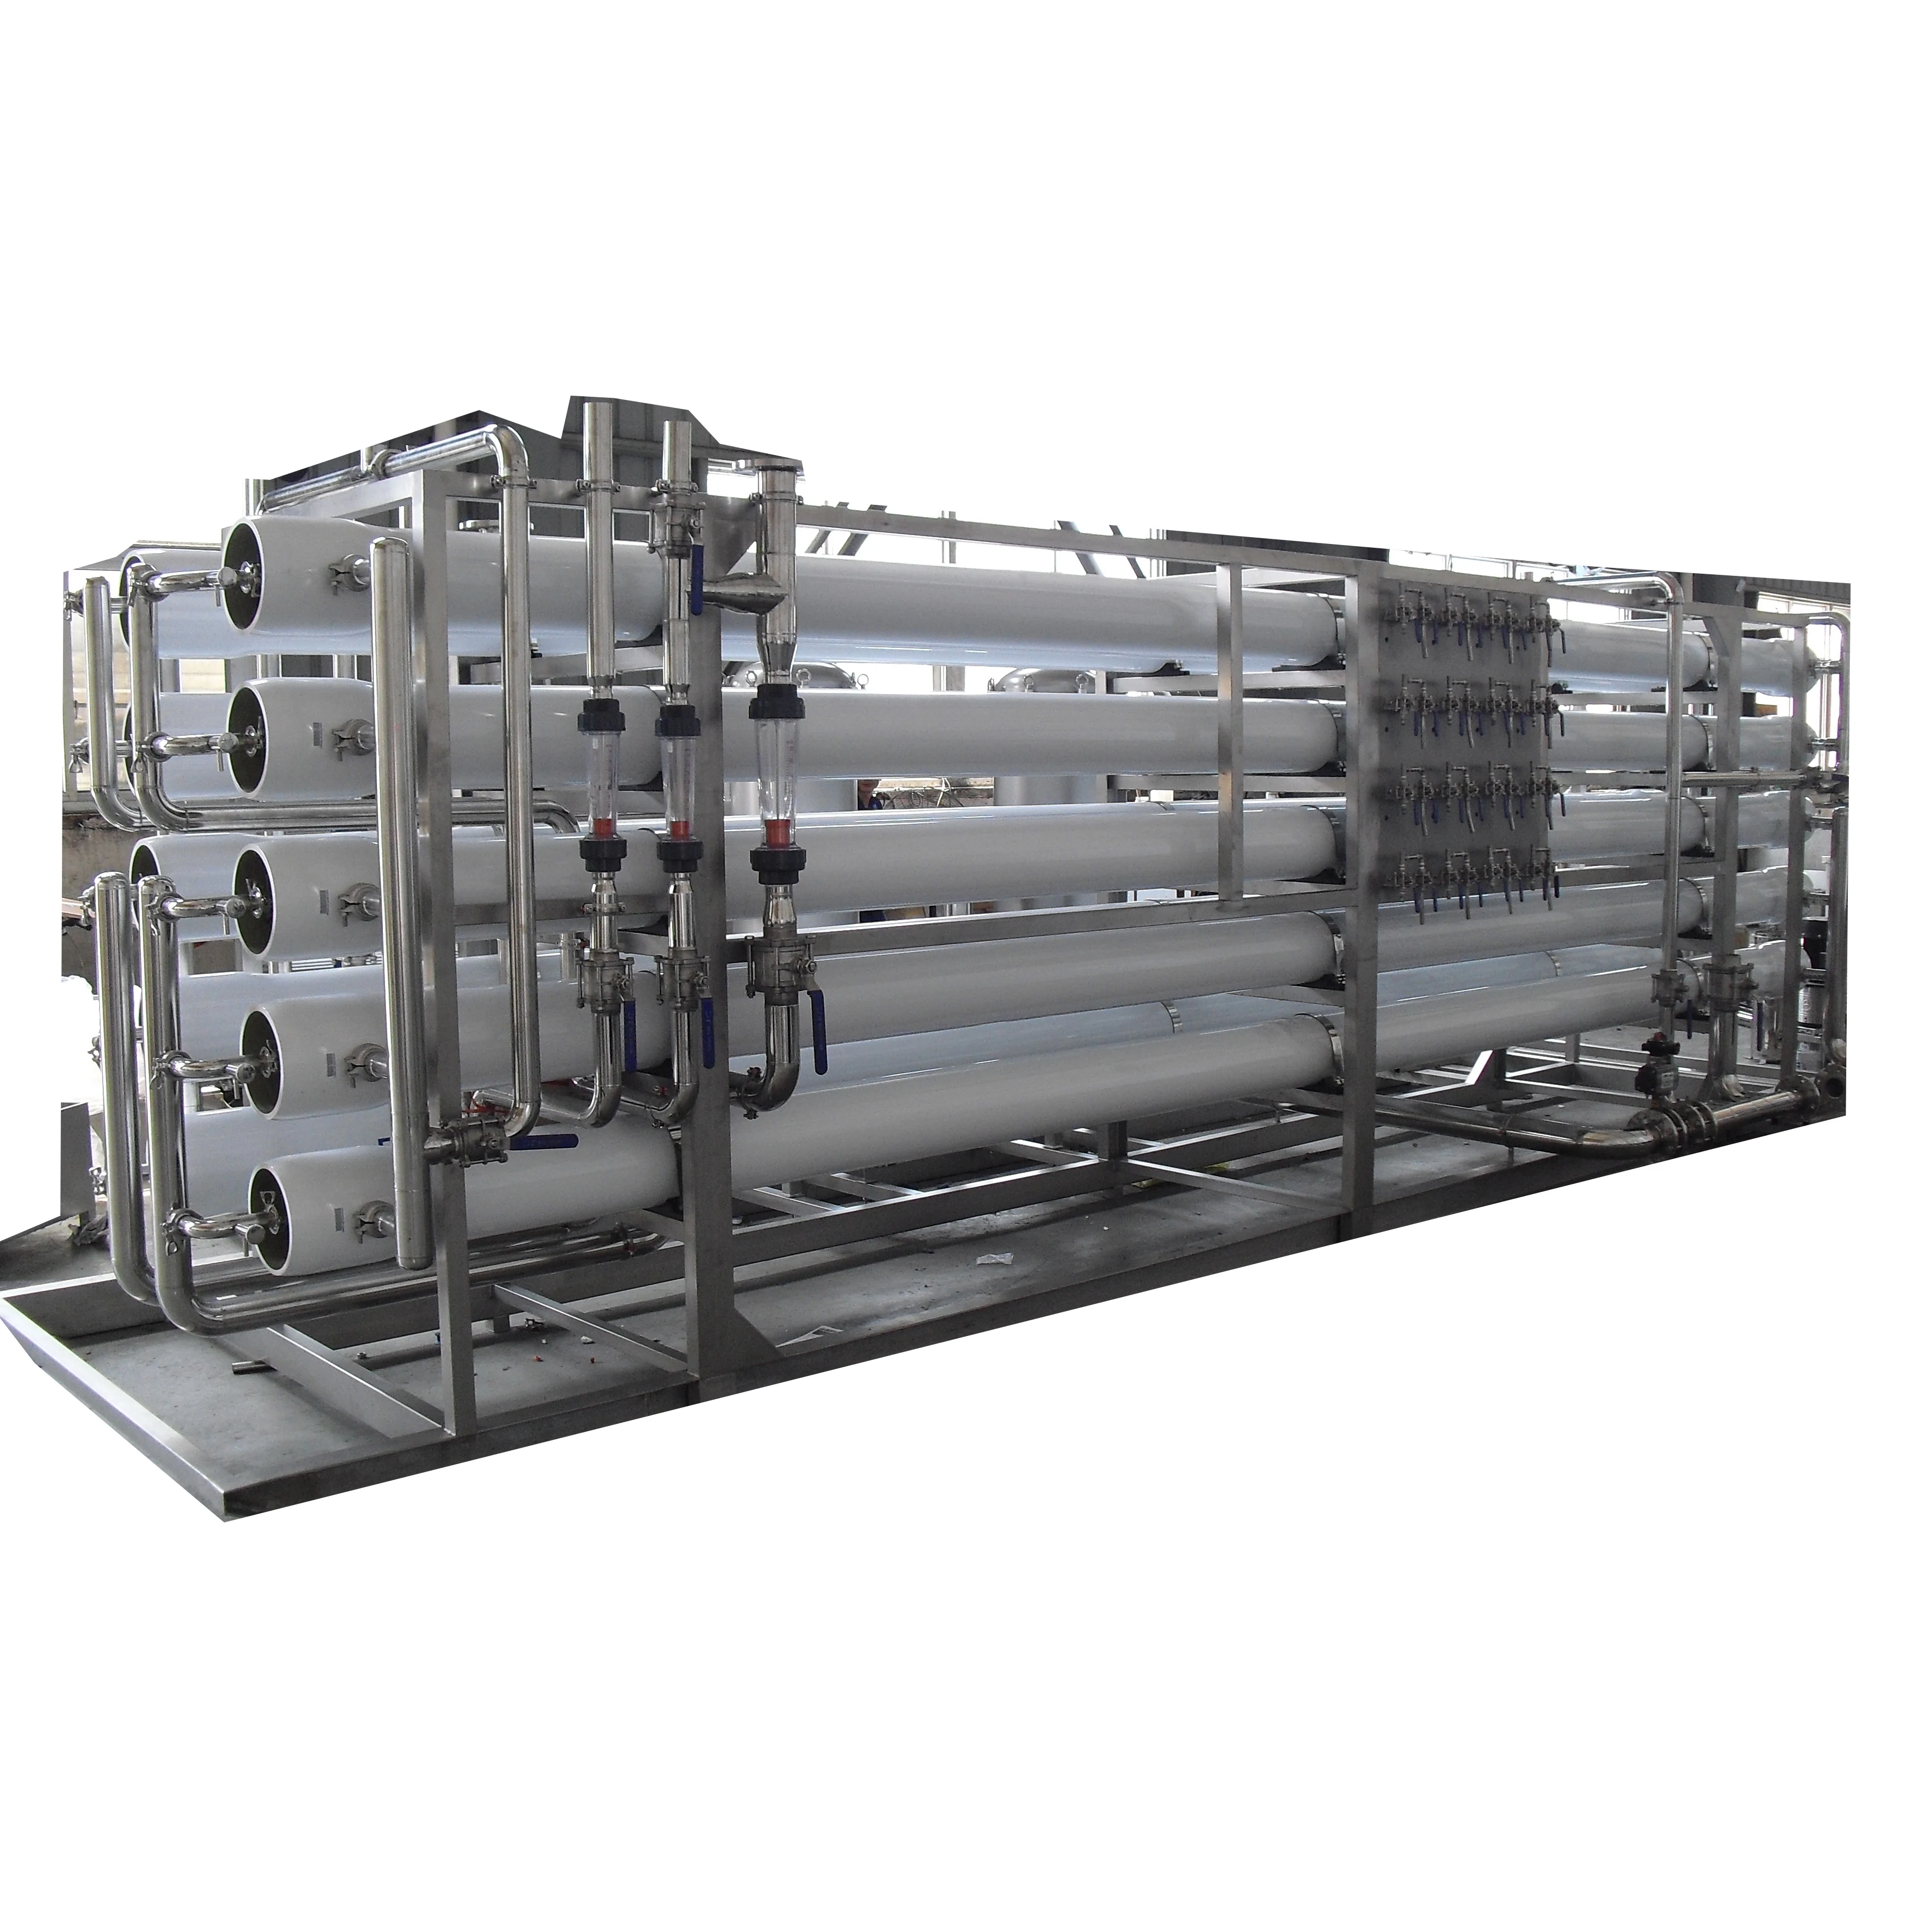
Investing in a water packing machine is a critical decision for businesses in the beverage industry. These ZPACK water packing machine play a vital role in ensuring the efficient packaging of water products, safeguarding their quality while optimizing production processes. However, potential buyers often face challenges in selecting the right machine, understanding specifications, and identifying trustworthy suppliers. This article aims to provide insights into choosing the appropriate water packing machine for your business needs, evaluating key specifications, sourcing suppliers, analyzing cost factors, and exploring applications across various industries.
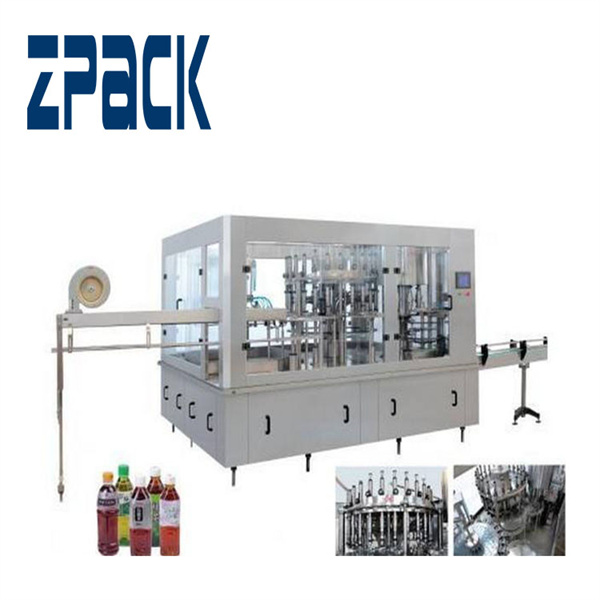
Selecting the appropriate water packing machine requires careful consideration of several factors. First, identify the specific requirements of your production line, including the type of water products you intend to package—whether bottled, bagged, or in bulk. Consider the production capacity you need, as this ZPACK automatic water packing machine will influence machine size and speed.
Moreover, evaluate the machine’s compatibility with your existing processes. For instance, if your facility already has a filling line, you’ll want a packing machine that seamlessly integrates with it. The level of automation is also essential; fully automated machines can enhance efficiency but may require a higher initial investment. Lastly, think about customization options. A ZPACK mineral water packing machine that can adapt to different packaging formats or sizes may provide greater flexibility as your business evolves.
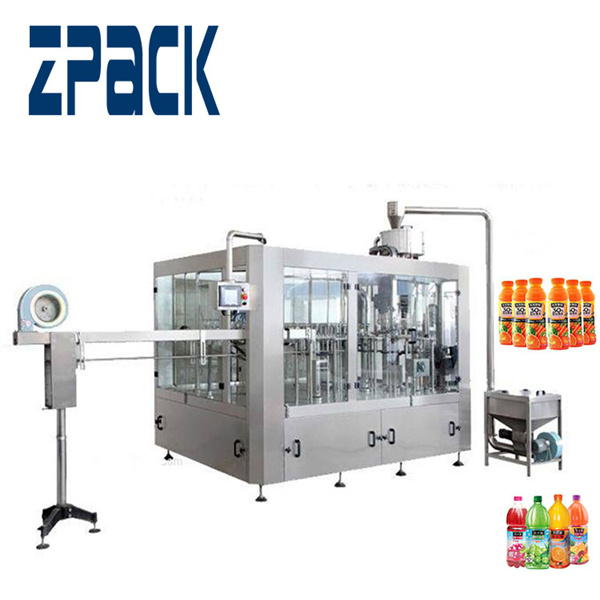
When evaluating water packing machines, several specifications are crucial for ensuring optimal performance and suitability for your needs. Key specifications to consider include:
Filling Speed: Measured in bottles per minute (BPM), this determines how quickly the machine can package water. Higher speeds are advantageous for large-scale operations but should be balanced with quality control.
Container Compatibility: Ensure the machine can accommodate the types of containers you plan to use, whether plastic bottles, glass, or pouches. This includes considerations for size and shape.
Sealing Mechanism: The sealing method (such as heat sealing, vacuum sealing, or cap sealing) affects the shelf life and safety of the packaged product. Choose a mechanism that meets your quality standards and regulatory requirements.
Control Systems: Advanced control systems can enhance precision and facilitate monitoring, making it easier to maintain production consistency. Look for machines with user-friendly interfaces that allow for easy adjustments.
Material Construction: The materials used in the machine’s construction should be durable and compliant with food safety standards. Stainless steel is commonly preferred for its resistance to corrosion and ease of cleaning.
Understanding these specifications will help you assess whether a water packing machine aligns with your operational requirements and quality expectations.
Sourcing a reliable water packing machine supplier is essential for ensuring product quality and support. Here are some practical tips for wholesale sourcing:
Research Suppliers: Begin with thorough research to identify suppliers with a solid reputation in the industry. Look for manufacturers with extensive experience in producing water packing machines and positive reviews from existing clients.
Evaluate Certifications: Check for relevant industry certifications, such as ISO 9001, which indicate adherence to quality management standards. Certifications can provide assurance about the manufacturer’s commitment to quality.
Request References: Don’t hesitate to ask potential suppliers for references from past clients. This can provide insight into their reliability, customer service, and the performance of their machines in real-world applications.
Assess Product Range: A supplier with a diverse range of water packing machines may offer better options for customization and scalability, allowing you to adapt to changing market demands.
Visit Facilities: If possible, arrange site visits to the manufacturer’s facility. This firsthand experience can help you assess their production capabilities, quality control processes, and overall professionalism.
By following these tips, you can enhance your chances of finding a trustworthy supplier that aligns with your business needs.
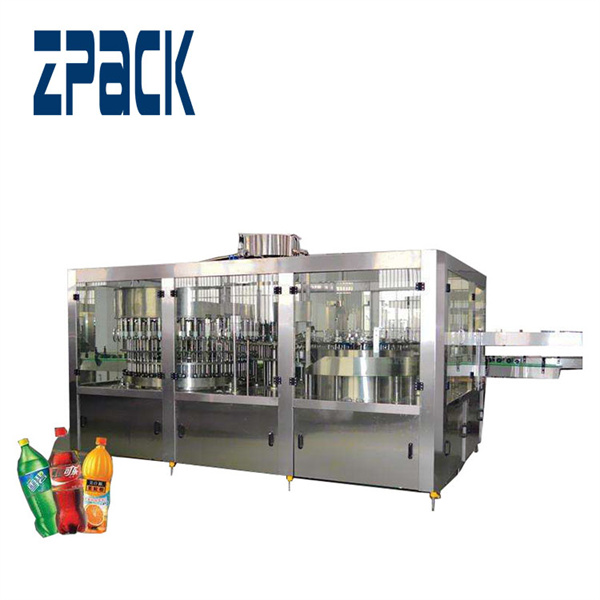
The cost of a water packing machine can vary significantly based on several factors. Understanding these cost factors will help you make an informed purchasing decision:
Machine Type and Features: Different types of machines (manual, semi-automatic, or fully automatic) come with varying price points. Additionally, features such as advanced control systems or specialized sealing techniques can impact costs.
Production Capacity: Higher capacity machines typically require a larger investment. Consider your production needs and balance them against your budget to find a machine that meets your requirements without overspending.
Customization: Custom features tailored to your specific packaging needs may increase the overall cost. While customization can enhance efficiency, it’s essential to evaluate whether these features are necessary for your operations.
Shipping and Installation Costs: Don’t forget to factor in shipping and installation expenses, which can add to the overall investment. Ensure you discuss these details with the supplier upfront to avoid unexpected costs.
Maintenance and Operating Costs: Consider the long-term costs associated with operating and maintaining the machine. Energy efficiency, ease of maintenance, and availability of spare parts can all influence these ongoing expenses.
By considering these cost factors, you can better assess your budget and make a more informed decision when purchasing a water packing machine.
Unwavering commitment to quality that protects your equipment with every step of the way. We recognize that a product's capabilities don't end after the purchase. We provide a comprehensive after sale to ensure customer satisfaction. We create an after-sales guarantee team for each customer, ensuring timely and efficient service. When any issues arise our team will address the issue within two hours and offer an solution within eight hours. We also provide a longer 5 gallon filling machine time, and our maintenance staff is always on hand to help with technical issues.
We provide competitive products as well as individualized custom-designed products The quality of our products is a top priority for us Our equipment undergoes extensive testing to ensure its flawless operation We utilize the most modern testing methods and follow strict standards of quality control in order to ensure our equipment is up to standards 3 in 1 liquid filling machine to delivering it to our clients
Specialized in the Active carbon filter of new equipment and providing solutions to clients across the world As a nationally recognized high-tech firm we are able to boast a formidable scientific and technological research and development strength Our team of experts are comprised of industry leaders and innovators who are always exploring the frontiers of technology to design innovative solutions Our products and services will remain in the forefront of technology allowing our customers to enjoy a a competitive advantage
Quality standards and stringent requirements are utilized in the manufacturing of equipment We can provide reasonable prices We pride 5 gallon bottle blowing machine on our ability to offer competitive prices without compromising on quality We eliminate middlemen and rely only on our physical manufacturing facility This avoids any unneeded price increases We can pass these savings to our customers and make sure they receive the best value
Water packing machines serve a variety of applications across multiple industries beyond the beverage sector. Here are some notable examples:
Beverage Industry: Primarily used for packaging bottled water, these machines are essential for ensuring product quality and safety. Their ability to handle various container types makes them versatile for different brands.
Food Industry: Water packing machines can also be used for packaging sauces, soups, and other liquid food products. Their precise filling capabilities ensure accurate portions, which is critical for maintaining consistency.
Pharmaceutical Industry: In the pharmaceutical sector, water packing machines are used to package sterile water for injections or other medicinal uses. The stringent hygiene requirements in this industry necessitate machines that comply with strict safety standards.
Chemical Industry: These machines can package liquid chemicals, ensuring safe and reliable containment. The choice of materials and sealing methods is crucial to prevent contamination and maintain product integrity.
Understanding the various applications of water packing machines can help businesses identify new opportunities for growth and diversification.
By addressing these key aspects, this article aims to empower B2B buyers with the necessary knowledge to make informed decisions regarding water packing machines, ensuring optimal productivity and product quality for their operations.
 EN
 AR
 BG
 NL
 FR
 DE
 EL
 HI
 IT
 JA
 KO
 PT
 RU
 ES
 TL
 IW
 ID
 SR
 VI
 SQ
 TH
 TR
 FA
 AF
 MS
 SW
 BE
 BN
 EO
 HA
 KM
 LA
 MN
 ZU
 UZ
 AM
 KU
 SD
 XH